Sieve Blinding and Mesh Selection for Fine Pharmaceutical Powders
Most blinding problems start as a mesh selection problem. Pick the aperture for the product, then solve blinding at the mesh instead of compromising the cut.
Why the Sieve Slows Down
Sieving rarely gets much attention on an equipment list. It is the quiet step between the mill and the blender, and it only gets noticed when it stops keeping up. When it does, the symptom is nearly always the same: the sieve ran fine on the first batch, throughput fell off over the shift, and an operator ended up stopping the line to brush the screen. That is blinding, and it is the most common reason a check screen that was sized correctly on paper underperforms on the floor.
Blinding happens when a particle, or a cluster of particles, sits on or in a mesh aperture and stays there. Every blocked opening is screening area you paid for and are no longer using, so capacity drops batch by batch. It is most common on screens of 300 microns and below, with powders that are sticky or light, and with powders that contain a lot of particles close to the aperture size. Fine pharmaceutical powders tend to be all three at once.
Three Ways a Mesh Blinds
It helps to know which kind of blinding you have, because the fixes are different.
| Mechanism | What is happening | Where you see it |
|---|---|---|
| Near-size wedging | Particles slightly larger or slightly smaller than the aperture lodge in the opening instead of passing or being rejected. | Any powder with a wide size distribution screened at an aperture inside that distribution. Milled and micronized material is the classic case. |
| Sticky or light powders | Particles adhere to the wires or to each other and build up across the openings. | Cohesive APIs and excipients, and low-density powders that are slow to settle onto the mesh. |
| Agglomerates | Soft lumps formed in storage or transfer sit on the mesh and block openings until they break down. | Excipients that cake, talc, and anything that picked up moisture between the drum and the sieve. |
The first mechanism is worth a closer look, because it is built into the job in one common pharmaceutical case. If a sieve is adjusting the particle size distribution of an API after milling, the aperture sits inside the distribution by definition. Near-size particles are not an accident there. They are the product. Powder that has just come off a mill or a jet mill is among the hardest material a sieve will see, and a line that sieves straight after size reduction should plan for deblinding from the first day, not after the first slowdown.
Start With What the Sieve Is For
Before any aperture gets written on a URS, decide which of two jobs the sieve is doing. The answer changes everything downstream.
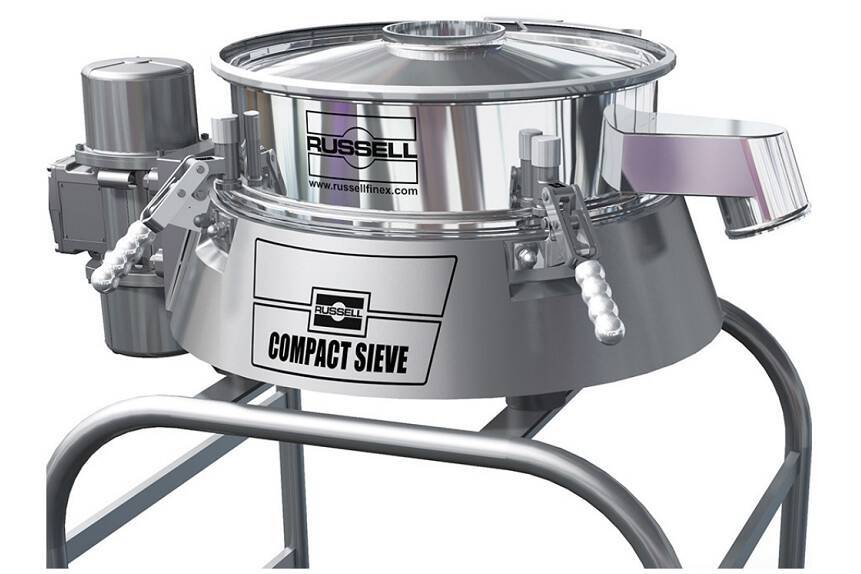
Check screening. The sieve is a quality control point. Its job is to catch what should not be there: oversize, foreign material, lumps, packaging debris, and the odd agglomerate. The product itself should pass freely. For this job the right aperture is the largest one that still catches what you need to catch, because every step finer than that adds blinding risk for no gain in protection. A standard Compact Sieve rated for 1,000 kg per hour of pharmaceutical powder on a 630 micron mesh is doing this job, and that aperture sits well above the range where blinding is common.
Grading or distribution adjustment. The sieve is making a cut inside the product. Its job is to hold the particle size distribution to a specification, and the aperture is set by the specification, not by what the mesh can tolerate. Here the question of “which mesh” has already been answered by the formulation. The real question is how to keep that mesh open.
Two practical notes on specifying the mesh itself. Write the aperture in microns, with the mesh count as a cross-reference, so there is no ambiguity about what was ordered: 635 mesh is 20 microns, 150 mesh is 100 microns, and the numbers only get confusing from there. And give the mesh frames somewhere to live between campaigns. Russell Finex offers a storage rack for exactly that reason: a dented frame is a torn mesh at the next changeover.
What Not to Do About It
Three fixes get tried first, and each costs something that matters in a GMP environment.
- Manual brushing. Stops the line, needs an operator in the product, and tends to damage or break the mesh. Worse, the product specification drifts with the degree of blinding between cleanings, so batch one and batch six were screened on different effective apertures.
- Tapping balls or discs under the mesh. These bounce against the screen to shake blockages free. They also wear the mesh, and as the balls or discs wear down, pieces of rubber or plastic can end up in the sieved powder. On a product contact surface that is a contamination source you installed on purpose. They are loud, too: some disc assemblies have been measured above 90 dB(A).
- A coarser mesh. Covered above. Acceptable on a check screen if the coarser aperture still does the quality job; not acceptable on a grading screen.
Solving It at the Mesh: Ultrasonic Deblinding
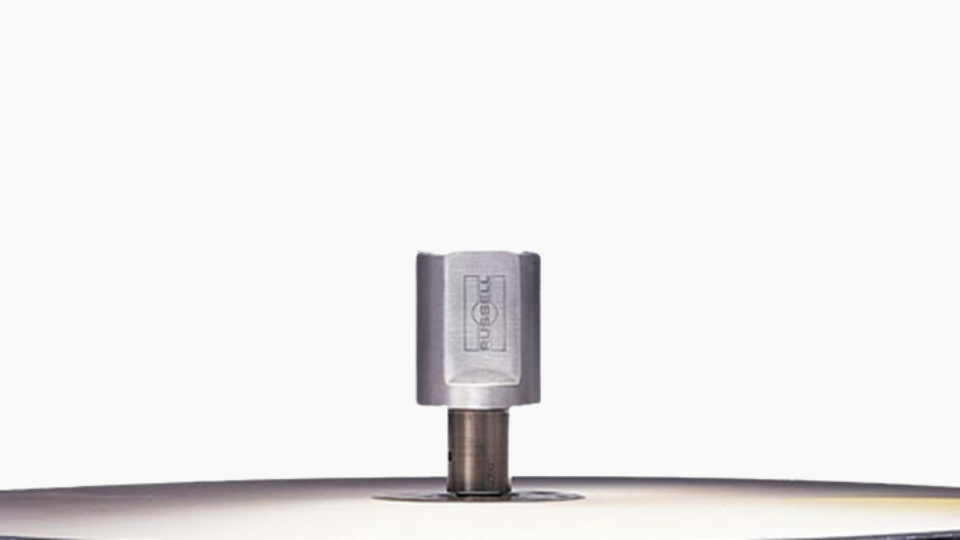
The fix that does not trade away the cut is to stop particles sticking to the wires in the first place. Russell Finex builds its own ultrasonic deblinding system, the Vibrasonic 2000, alongside the sieves it fits to, and the pairing is the standard answer for fine pharmaceutical powders on a Compact Sieve.
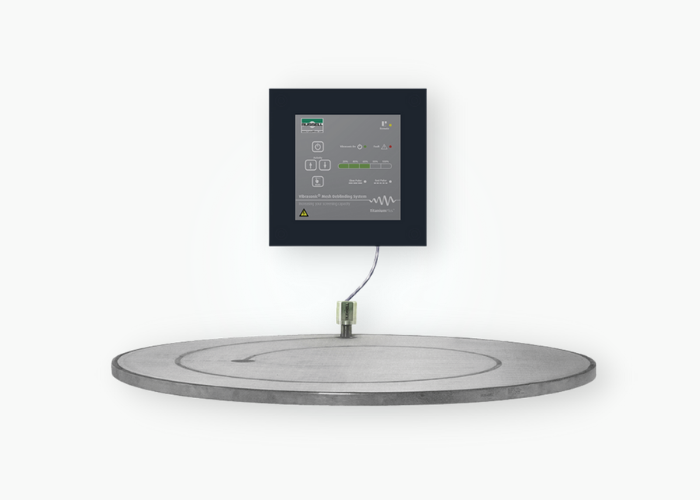
The system has three parts. A control unit drives a piezoelectric probe at its resonant frequency of 35 kHz. The probe bolts to a velocity transfer plate that is bonded to the stainless steel wires of the mesh, so the ultrasonic energy goes into every individual wire. At that frequency the wires behave as if they were friction-free, and particles slightly above or below the aperture size stop lodging in the openings. Everything that should pass, passes; everything that should be rejected moves off the screen.
What that changes in practice:
- Capacity stays constant through the shift. The screening area that was open at the start of the batch is still open at the end, so there is nothing to clean and no slow decline to compensate for.
- Finer screening becomes a production operation. Accurate screening below 100 microns at production scale was close to impossible with conventional deblinding. With ultrasonics, apertures down to 20 microns (635 mesh) are achievable.
- Nothing wears and nothing sheds. There are no mechanical parts touching the mesh, so no mesh damage from the deblinding device and no foreign material from it.
- Mesh life goes up. With manual cleaning gone, the most common cause of mesh breakage goes with it.
- It can be tuned to the powder. Light powders can bounce off a mesh that is driven too hard. The control unit can pulse the activity in short bursts, or modulate it, so the powder settles and screens between pulses and any blinding is cleared when the activity returns.
Russell Finex’s own capacity table shows the pattern. Every dry powder listed at 100 microns or finer runs with a Vibrasonic system: toner at 75 microns, stainless steel powder at 42 microns, powder paint and tungsten carbide at 100 microns. The pharmaceutical powder example on the same table runs at 630 microns with no deblinding at all. That is the whole argument in one table. At coarse check-screening apertures the sieve stands on its own; as the aperture drops toward and below 100 microns, the deblinding system is what makes the mesh usable.
Two pharmaceutical cases from Russell Finex’s published work show the same thing on real product. An API manufacturer that mills and jet mills fine particles, and had no suitable equipment for removing mechanical impurities, paired a Compact Sieve with a Vibrasonic system to adjust API particle size distribution to customer specifications; the line now processes 100 to 400 kg per shift. A sterile API manufacturer screening microsphere powder at 71 microns was limited to 1.5 kg per hour on a small ultrasonic sifter. Moving to a Compact Sieve with a side-mounted ultrasonic probe took screening capacity to 10 kg per hour, and cut operator handling by 30 to 40 percent along the way.
Where the Set-up Matters
The ultrasonic system can be specified new or retrofitted to an existing sieve, including sieves of other makes, on almost any diameter up to two metres. That flexibility comes with one caution worth knowing before a retrofit. Most vibratory sieves have adjustable weights on the motor that set the amplitude of vibration and the speed material travels across the screen. After adding ultrasonics those weights usually need resetting: if the amplitude is too high the powder is not in constant contact with the mesh and the ultrasonic system cannot work at full efficiency. Getting the two technologies to complement each other is a set-up task for an engineer who knows both, which is the practical reason the pairing works best when one manufacturer builds both halves.
Two further options are worth asking about on a fine-powder application. The Spiroscreen variant adds a spiral guidance path on the mesh, which controls how the powder moves across the screen, keeps the ultrasonic activity close to the powder, and improves separation accuracy. And both the sieve and the deblinding system are available in ATEX-approved versions for dust zones, which many fine organic powders require.
The Honest Answer to “Which Mesh”
The aperture comes from the job, as above. Whether that aperture runs cleanly on your powder is not something a data sheet can tell you, because blinding depends on particle shape, moisture, cohesion, and the shape of the size distribution, none of which appear in a capacity table. The only reliable answer is to run the actual powder on the actual mesh, with and without ultrasonics, and measure throughput over time rather than at minute one. Russell Finex offers that as a trial, either at a test facility or at the customer plant, and we arrange it as a matter of course before a fine-powder sieve is specified.
Related Pages
- Russell Finex: sieving and screening equipment for pharmaceutical powders
- Russell Compact Sieve: the check screener the Vibrasonic system fits to
- Russell Compact Airlock Sieve: the high-containment version for potent compounds
- Russell Compact Airswept Sieve: check screening inside a vacuum conveying line
- Inline sieving after bowl inversion: where a check screen sits in a powder workflow
Sieving a Fine Powder That Blinds?
MHS Pharma represents Russell Finex across the Northeast United States. We can help you settle the aperture, decide whether ultrasonic deblinding belongs on the specification, and set up a trial on your own powder.
Contact MHS Pharma